Address:
Shenzhen Bao'an District Xinqiao Subdistrict Huangpu Community Huangpu East Ring Road No. 504 Shenzhen Yuan Industrial City Building C
Work Hours:
Monday to Friday: 9AM - 21PM
Weekend: 9AM - 21PM
Address:
Shenzhen Bao'an District Xinqiao Subdistrict Huangpu Community Huangpu East Ring Road No. 504 Shenzhen Yuan Industrial City Building C
Work Hours:
Monday to Friday: 9AM - 21PM
Weekend: 9AM - 21PM
Titanium CNC machining for orthopedic implants plays a critical role in developing precision medical hardware that must conform to complex human anatomy and withstand long-term mechanical loading. For engineering teams evaluating 5 axis cnc machining tolerances for medical devices, the challenge extends beyond producing accurate dimensions. Implant prototypes must combine biocompatible materials, complex anatomical geometry, controlled surface integrity, fatigue resistance, and documented manufacturing quality.
During new product introduction (NPI), orthopedic implants such as hip stems, spinal fusion cages, fixation plates, and specialized joint components require increasingly sophisticated manufacturing methods.
Traditional three-axis machining may require multiple setups to access complex surfaces. Each repositioning introduces potential datum-transfer errors, while inappropriate toolpaths can leave undesirable surface transitions.
Five-axis CNC machining offers a flexible solution through simultaneous tool-axis movement, improved access to complex geometries, and fewer setups.
For Orthopedic R&D Engineers, Biomedical Engineers, Senior Mechanical Engineers, Quality Managers, and Procurement Managers, understanding these capabilities is essential for reducing development risk.
This guide covers material selection, anatomical machining, GD&T, CNC versus metal 3D printing, DFM cost optimization, cleaning requirements, and the complete development process from CAD → prototype samples → functional validation → low-volume pilot production → mass production support.
Medical implants present manufacturing challenges that differ significantly from conventional industrial components.
An orthopedic implant may need to:
Match complex anatomical geometry
Maintain precisely positioned fixation interfaces
Withstand repeated loading
Support stable mechanical fixation
Meet demanding surface requirements
Use appropriately specified implant materials
Unlike simple brackets or housings, implant designs frequently contain multiple curved surfaces, angled holes, and functional interfaces.
A conventional three-axis machining center moves the cutting tool along three linear axes. Although advanced fixturing and multiple setups can produce complicated shapes, tool accessibility may become a limitation.
Five-axis CNC machining adds two rotational axes, enabling more flexible tool orientation.
Five-axis machining offers several potential benefits:
Improved tool accessibility: Angled features and accessible anatomical contours can be machined without extensive repositioning.
Reduced setup variation: Multiple critical surfaces may be machined while maintaining a common workholding reference.
Improved surface consistency: Appropriate tool orientation can reduce visible transitions between adjacent machined surfaces.
More efficient tooling: Tilting the tool may allow shorter, more rigid cutters to reach certain geometries.
However, five-axis machining does not automatically guarantee higher accuracy than three-axis machining. Machine calibration, toolpaths, fixturing, materials, and inspection remain essential.
Its main advantage is the ability to manufacture complex relationships more efficiently and consistently.
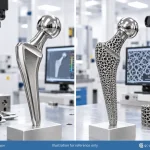
Titanium cnc machining for orthopedic implants is particularly valuable when producing complex orthopedic components from wrought Ti-6Al-4V ELI, commonly known as Grade 23 titanium.
This material offers high strength-to-weight performance, corrosion resistance, and established use in appropriately specified surgical implant applications.
ASTM F136 addresses wrought Ti-6Al-4V ELI material for surgical implant applications, including chemical, mechanical, and metallurgical requirements.
Potential applications include:
Hip stems
Orthopedic fixation plates
Spinal fixation components
Implant positioning interfaces
Patient-specific implant prototypes
Some orthopedic components require smoothly varying three-dimensional surfaces.
Examples include curved fixation plate interfaces and selected femoral or joint-related geometries.
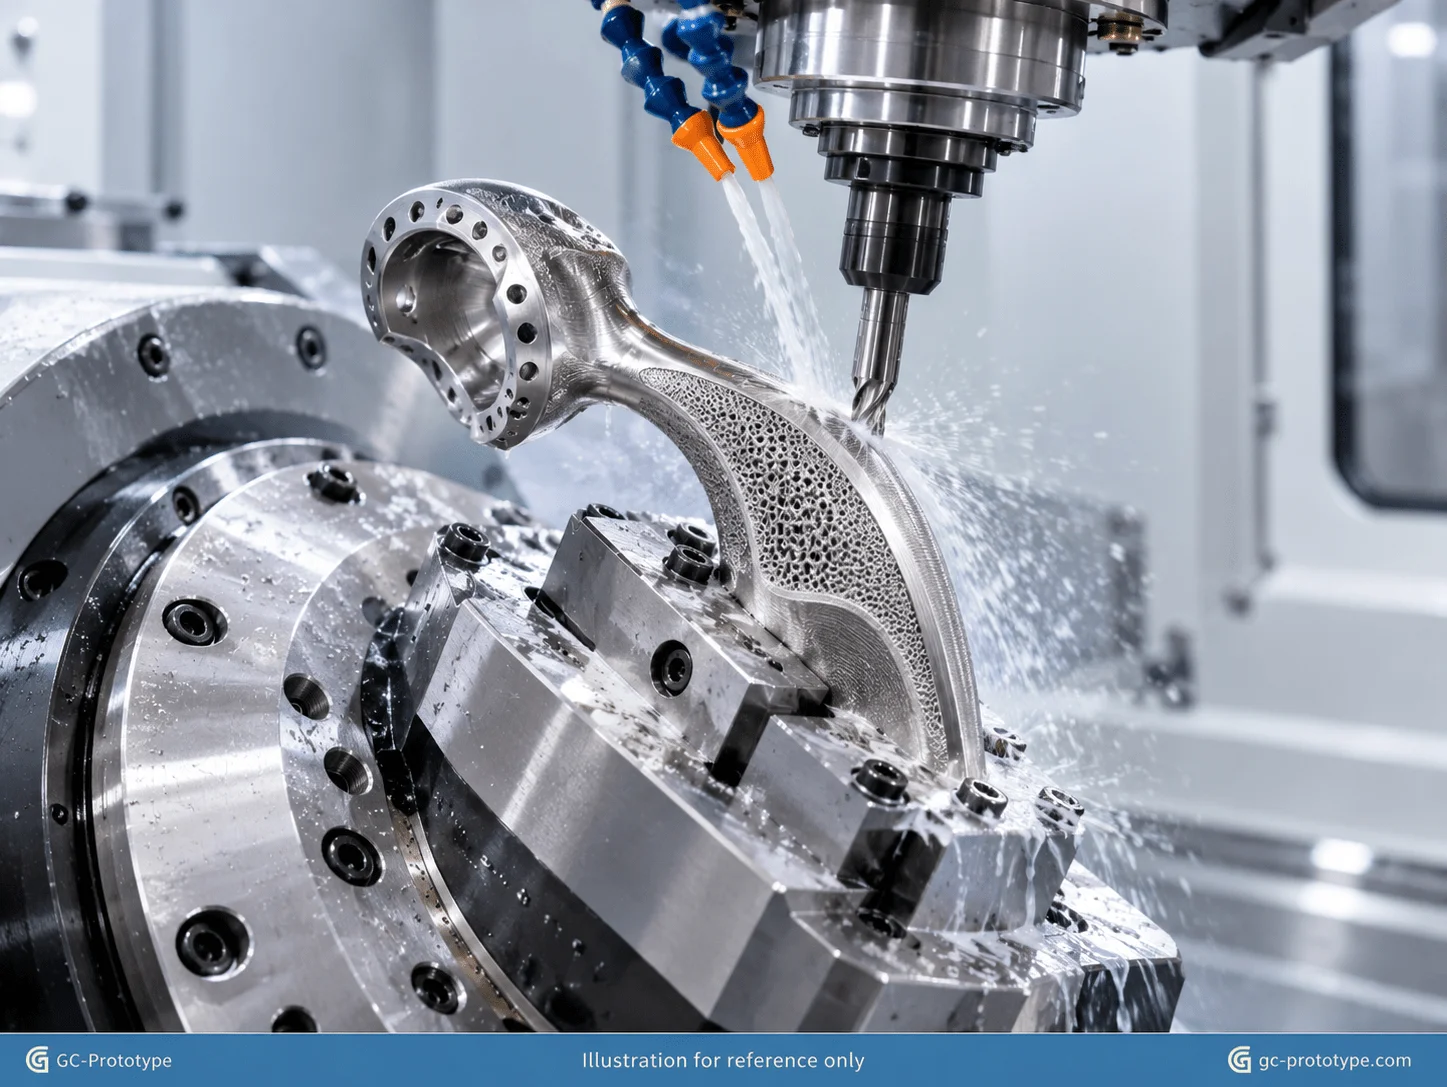
Five-axis milling can adjust tool orientation relative to these surfaces, improving access and allowing engineers to select suitable regions of the cutting tool for finishing.
A carefully programmed toolpath can help reduce:
Excessive cutting forces
Tool deflection
Surface irregularities
Unnecessary repositioning
Risk of unintended gouging
Titanium’s relatively low thermal conductivity introduces additional machining challenges.
Heat can concentrate around the cutting edge, accelerating tool wear and increasing the risk of surface damage.
Effective strategies include appropriate tool geometry, controlled engagement, reliable chip evacuation, and suitable cooling.
For fatigue-critical implants, surface integrity must also be verified. Five-axis machining alone cannot guarantee freedom from microcracks or a particular fatigue life.
Custom peek machining for spinal implants provides another important manufacturing route when engineers require high-performance polymer components for spinal fusion and related orthopedic applications.
PEEK, or polyether ether ketone, is a high-performance thermoplastic known for:
Radiolucency
Chemical resistance
Relatively low density
Good mechanical performance
Suitability for certain implant applications when the correct material grade is used
ASTM F2026 provides material requirements and testing considerations for PEEK polymers intended for surgical implant applications.
Spinal fusion cages may contain:
Anatomically shaped contact surfaces
Serrated fixation features
Internal bone-graft windows
Angled external faces
Complex insertion interfaces
Five-axis machining can improve access to multiple external surfaces and certain internal features, depending on tool accessibility.
PEEK requires a different machining strategy from titanium.
Because polymers have lower stiffness and thermal conductivity than most metals, cutting heat and clamping forces can cause temporary deformation.
Appropriate machining practices include:
Sharp cutting tools
Controlled cutting temperatures
Stable workholding
Suitable finishing allowances
Temperature-stabilized inspection
PEEK’s radiolucency can help clinicians assess surrounding structures using appropriate imaging methods.
CNC machining does not inherently remove this material property.
However, engineers must control contamination, embedded metallic debris, thermal damage, and surface defects.
The exact polymer grade, supplied stock, and subsequent processing should meet the applicable device specification.
Unfilled PEEK, reinforced PEEK, and implant-grade PEEK should not be treated as interchangeable materials.
Selecting the right material is one of the earliest decisions in medical implant development.
| Engineering Factor | Ti-6Al-4V ELI Titanium | Implant-Grade PEEK |
| Material Type | Metal alloy | High-performance polymer |
| Density | Higher | Lower |
| Strength | Very high | Lower than titanium |
| Elastic Modulus | Higher | Lower |
| Radiolucency | Limited | Excellent |
| CNC Machinability | Challenging | Good with proper controls |
| Thermal Conductivity | Relatively low for a metal | Very low |
| Typical Applications | Fixation hardware, orthopedic components | Spinal cages, selected implant components |
| Material Cost | High | High |
Titanium may be preferred where substantial structural strength and metallic fixation performance are required.
PEEK may be attractive for spinal applications where radiolucency, polymer mechanical characteristics, and the intended device design support its use.
Material selection must be based on engineering validation and device-specific regulatory requirements rather than a general assumption that one material is superior.
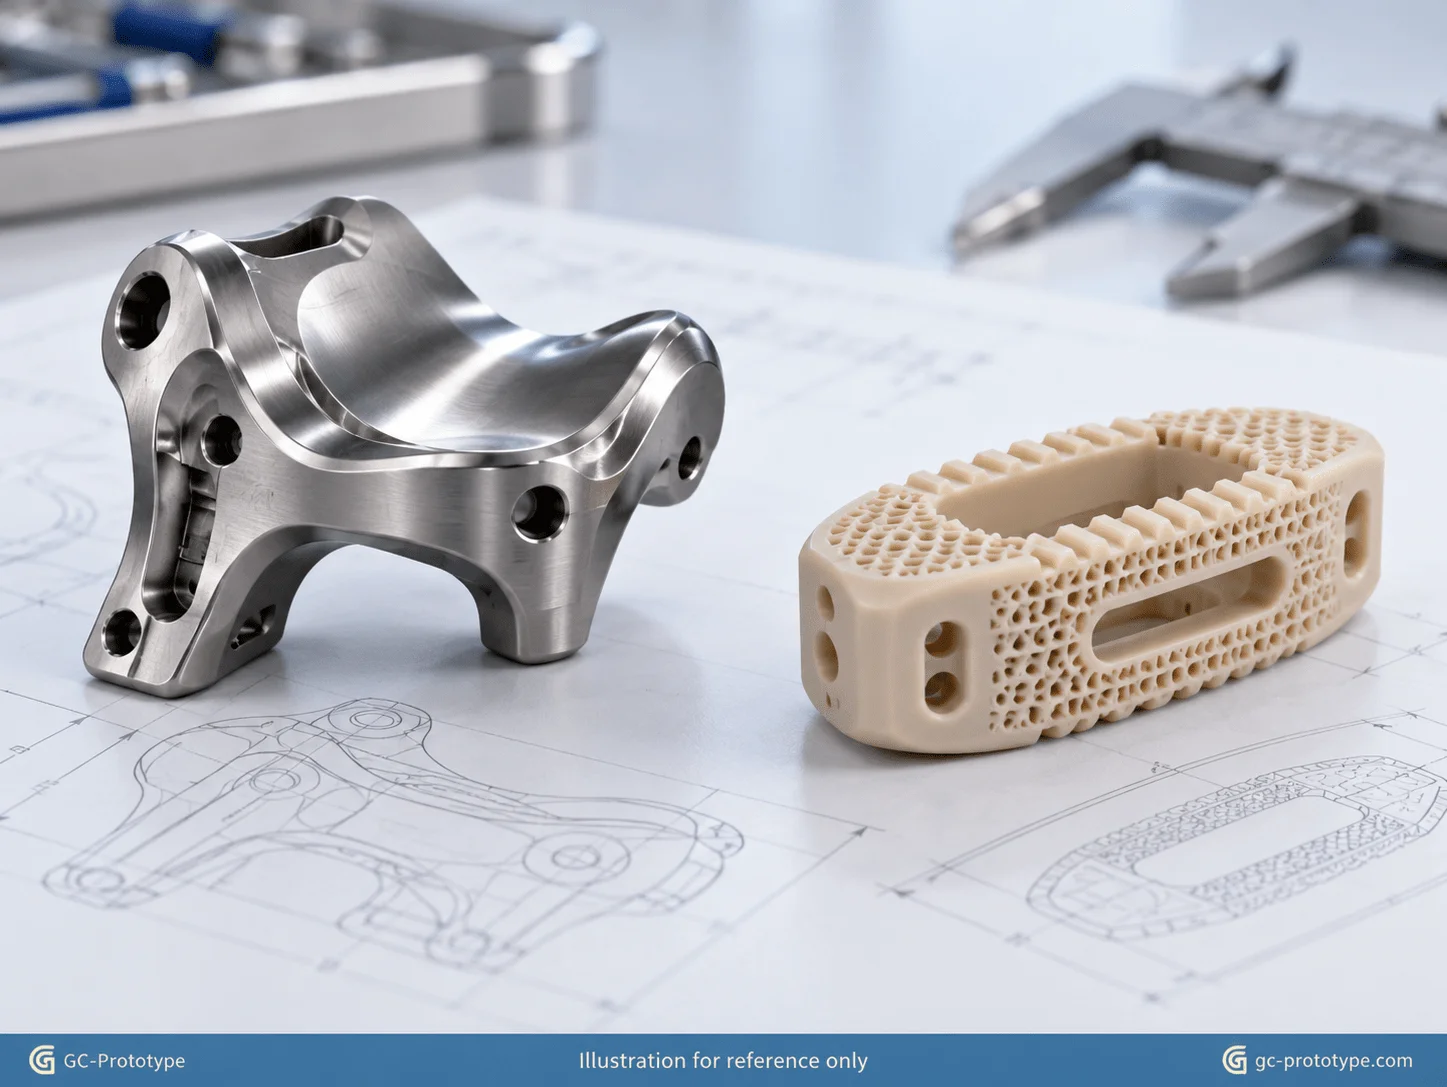
Achieving 5 axis cnc machining tolerances for medical devices requires coordinated control of machine accuracy, cutting forces, tool wear, thermal stability, and inspection.
Implant components frequently contain critical geometric relationships between:
Fixation holes
Curved contact surfaces
Mating interfaces
Locating features
Internal cavities
Angled screw trajectories
These features may require tighter geometric controls than ordinary industrial components.
Consider an orthopedic component containing three angled fixation holes and a curved reference surface.
With conventional machining, the manufacturer may need several setups to orient each feature.
Every repositioning creates potential variation in:
Location
Angular orientation
Datum alignment
Fixture repeatability
A five-axis machine may complete several of these operations without removing the component from its fixture.
This can reduce cumulative repositioning errors.
However, one setup does not eliminate all sources of variation. Rotary-axis calibration, workholding deflection, and thermal drift must still be controlled.
For certain highly demanding implant features, engineers may investigate tolerances around 0.005–0.008 mm.
These should be treated as feature-specific targets—not universal capabilities.
Importantly, GD&T profile tolerances are generally specified as total tolerance-zone values rather than automatically expressed as ± dimensions.
| Feature | Potential Engineering Control | Manufacturing Priority |
| Fixation hole | Position tolerance | Critical |
| Curved implant surface | Surface profile | Critical |
| Mating interface | Flatness or profile | Critical |
| Angled hole | Position and orientation | High |
| Nonfunctional exterior | General tolerance | Lower |
Achievable accuracy depends on component size, material, equipment, machining conditions, and inspection capability.
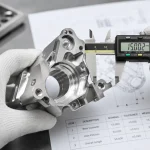
Measurement methods may include:
Coordinate Measuring Machines
Optical inspection
Surface profilometry
Precision gauges
Validated scanning systems
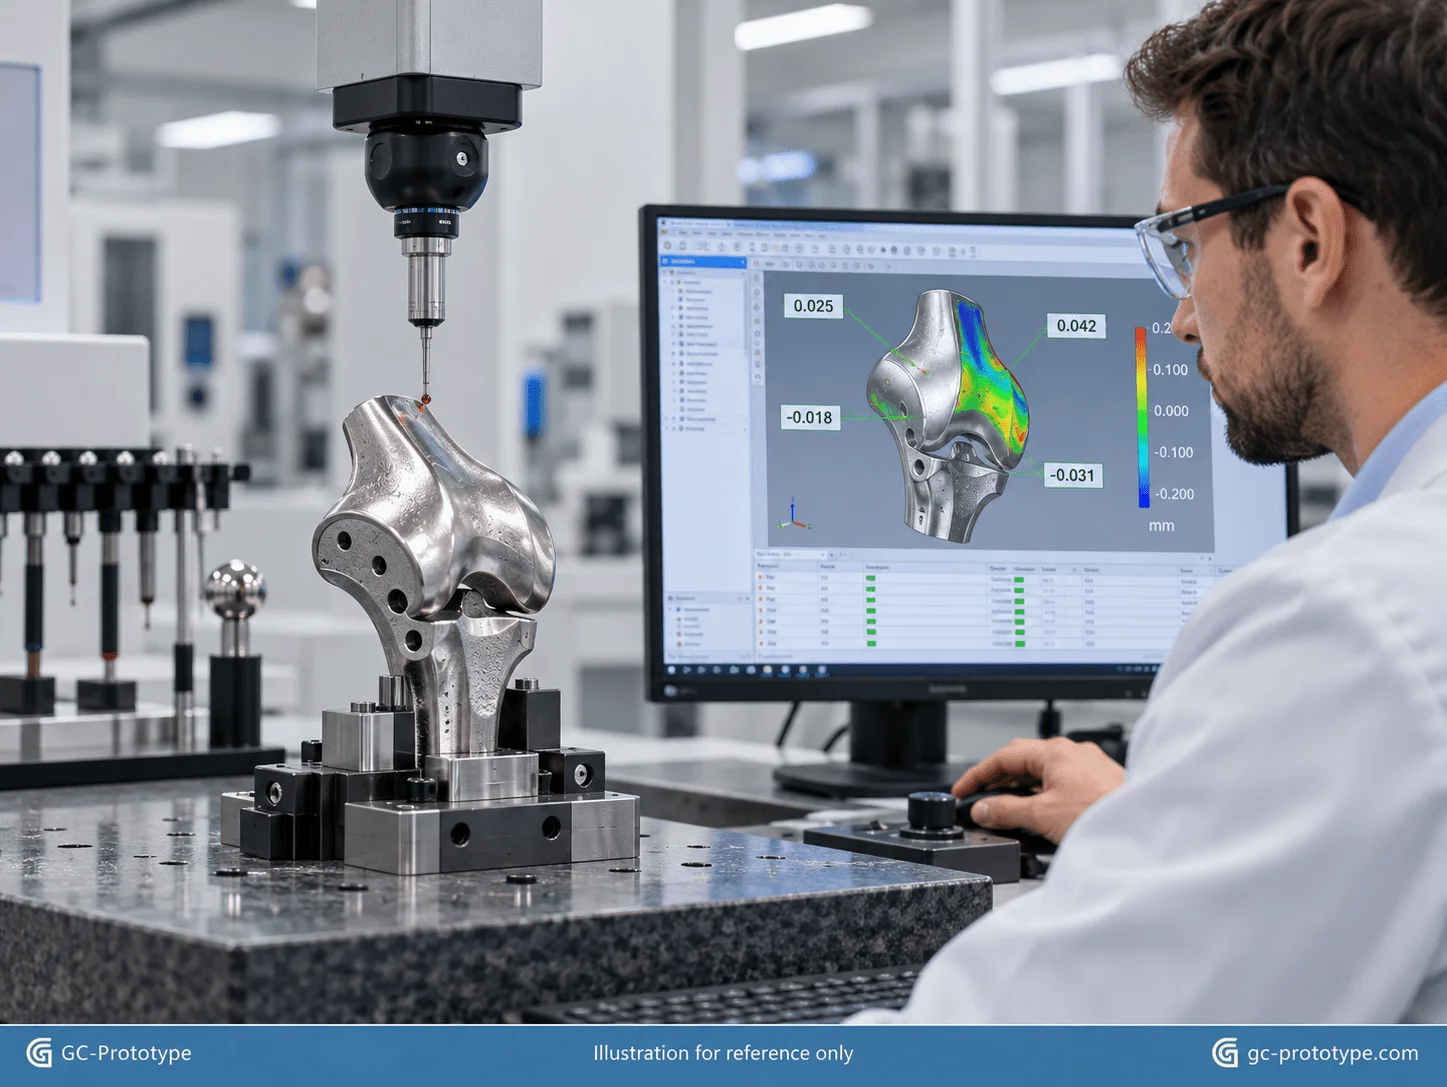
For complex anatomical surfaces, a CMM or suitable optical measurement system can compare manufactured geometry with the nominal CAD model.
The inspection plan should clearly identify the datum structure and functional requirements.
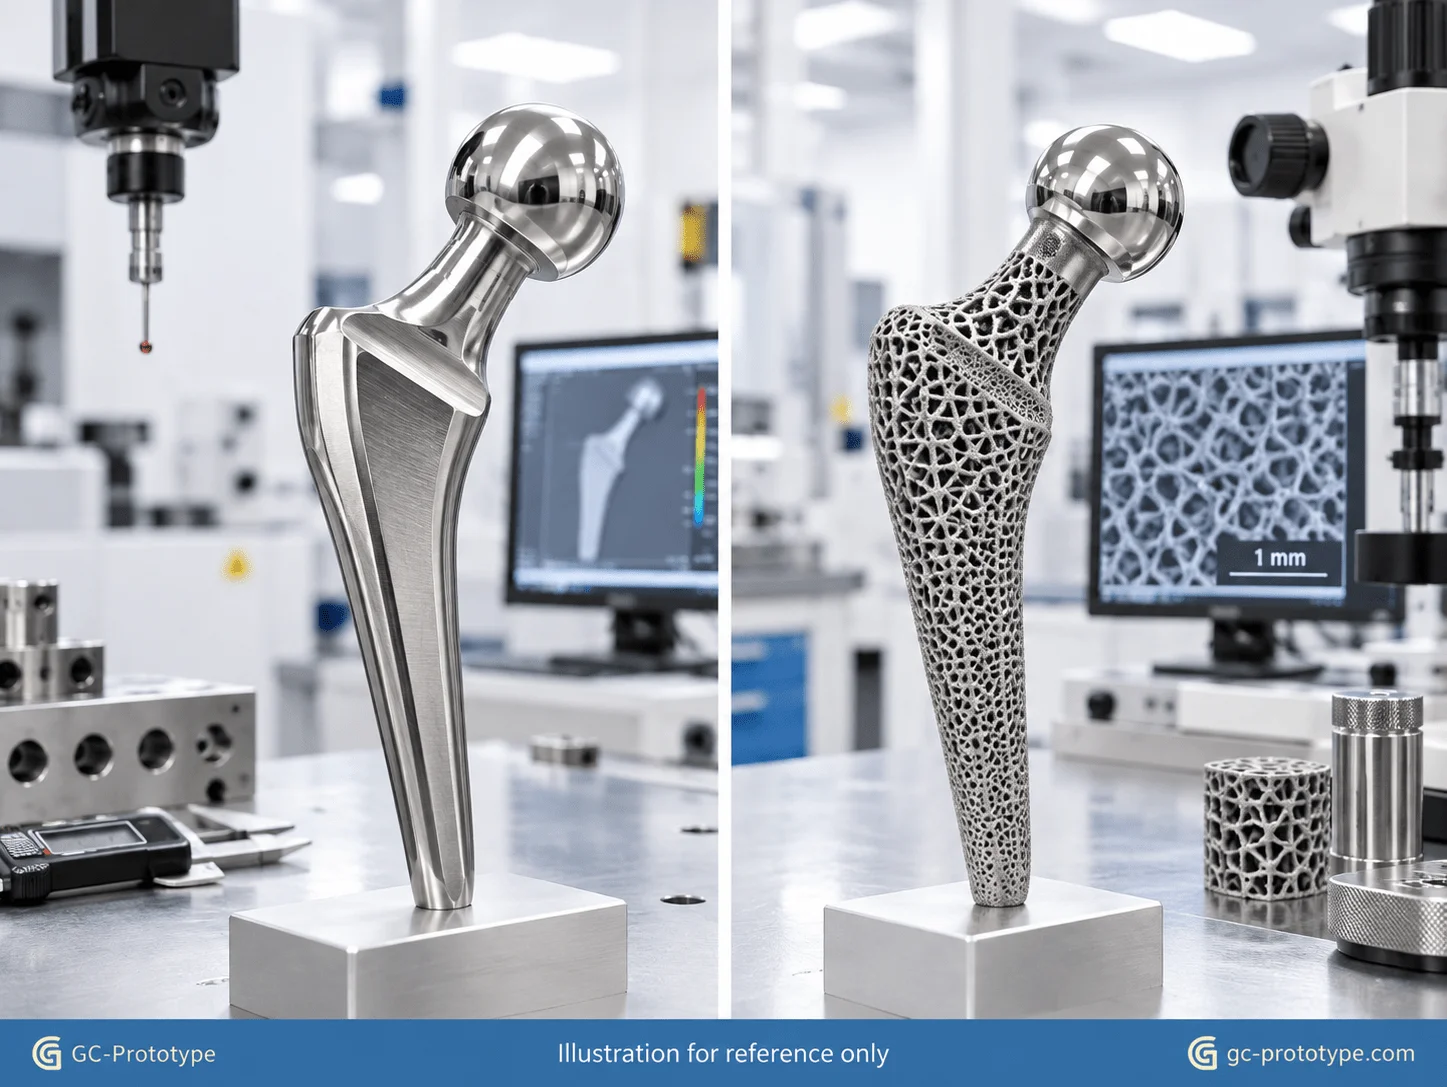
Comparing 5 axis cnc prototyping vs 3d printing for implants requires engineering teams to identify whether the prototype must validate precise interfaces, structural performance, complex porosity, or a combination of these requirements.
Both technologies can produce functional medical components.
Five-axis CNC machining is especially useful when producing parts from solid wrought or forged stock with accurately machined interfaces.
Metal additive manufacturing can create highly complex geometries, including porous structures and lattice features that are difficult or impossible to manufacture through conventional subtractive machining alone.
| Evaluation Factor | Five-Axis CNC Machining | Metal 3D Printing |
| Material Feedstock | Solid stock | Metal powder or other AM feedstock |
| Complex Internal Lattices | Limited | Excellent |
| Tight Interfaces | Excellent | Often requires finish machining |
| Surface Finish | Excellent | Often needs post-processing |
| Material Waste | Higher for complex shapes | Often lower |
| Mechanical Properties | Depend on wrought material and direction | Depend on AM process and post-processing |
| Porous Implant Features | Difficult | Strong advantage |
| Prototype Quantity | Suitable for 1–20 units | Suitable for 1–20 units |
CNC-machined parts from qualified wrought stock can provide predictable material properties when material condition, machining, and surface finishing are appropriately controlled.
However, wrought material is not necessarily perfectly isotropic.
Similarly, high-quality metal additive manufacturing can achieve excellent mechanical performance when supported by controlled processing, heat treatment, hot isostatic pressing where appropriate, and validation.
For implant applications, neither manufacturing method should be assumed to provide superior fatigue performance without appropriate testing.
CNC machining is often particularly attractive for:
Precision threaded interfaces
Closely controlled mating surfaces
Bearing or locating features
Smooth polished surfaces
Solid mechanical test specimens
For selected polished interfaces, surface roughness targets such as Ra ≤ 0.1 µm may be relevant, but these typically require suitable finishing operations and verification.
They should not be applied universally to implant surfaces.
Metal 3D printing is especially useful for:
Porous structures
Complex internal lattices
Patient-matched geometries
Designs with inaccessible internal features
The FDA’s guidance on additively manufactured medical devices addresses design, process validation, material controls, post-processing, and testing considerations.
A hybrid process is also possible: additive manufacturing creates the complex geometry, while CNC machining produces the critical precision interfaces.
Medical implant prototyping often uses expensive materials and demanding inspection processes.
The cost of a prototype can therefore rise quickly when its design contains unnecessary manufacturing complexity.
Effective DFM begins by identifying which features are essential to implant function.
Small internal corner radii require smaller cutting tools.
Small tools may increase:
Cycle time
Deflection
Chatter risk
Tool wear
Where the design allows, larger radii can improve manufacturing efficiency.
Complex anatomical features may require long tools to access deep regions.
Long tool overhang increases the risk of vibration and dimensional instability.
A suitable five-axis tool orientation can sometimes allow a shorter cutter to reach the same feature.
This can improve surface consistency and reduce finishing time.
Repeatable fixtures, zero-point clamping systems, and modular workholding can reduce preparation time between operations.
For prototype programs with multiple revisions, repeatable fixturing can be particularly valuable.
However, clamping strategy must also prevent deformation of thin titanium or PEEK features.
Not every feature requires micrometer-level accuracy.
Engineering teams should prioritize critical:
Fixation interfaces
Mating surfaces
Alignment features
Noncritical geometry can often use broader tolerances without compromising function.
This reduces unnecessary machining and inspection effort.
Implant manufacturing requires more than dimensional conformity.
Surface contamination, burrs, embedded particles, and machining residues may affect downstream validation.
A controlled finishing process may involve:
Precision deburring
Ultrasonic cleaning where appropriate
Validated chemical cleaning
Surface inspection
Protective packaging
Titanium and stainless steel do not necessarily require identical surface treatments.
Citric-acid passivation is associated with certain stainless-steel processing specifications and should not automatically be selected as the treatment for titanium implants.
For titanium, the appropriate process may involve validated cleaning, surface conditioning, or other device-specific treatments.
Ultrasonic cleaning can assist in removing residues, but it does not establish sterility or prove the absence of all contaminants.
Medical-device projects may require:
Material certificates
Lot traceability
Inspection reports
First Article Inspection
Process records
Cleaning validation documentation
ISO 13485 establishes medical-device quality-management-system requirements. In the United States, the FDA’s Quality Management System Regulation became effective on February 2, 2026, incorporating ISO 13485:2016 by reference.
A supplier’s ISO 13485 certification should be independently verified; component machining alone does not certify a finished medical device.
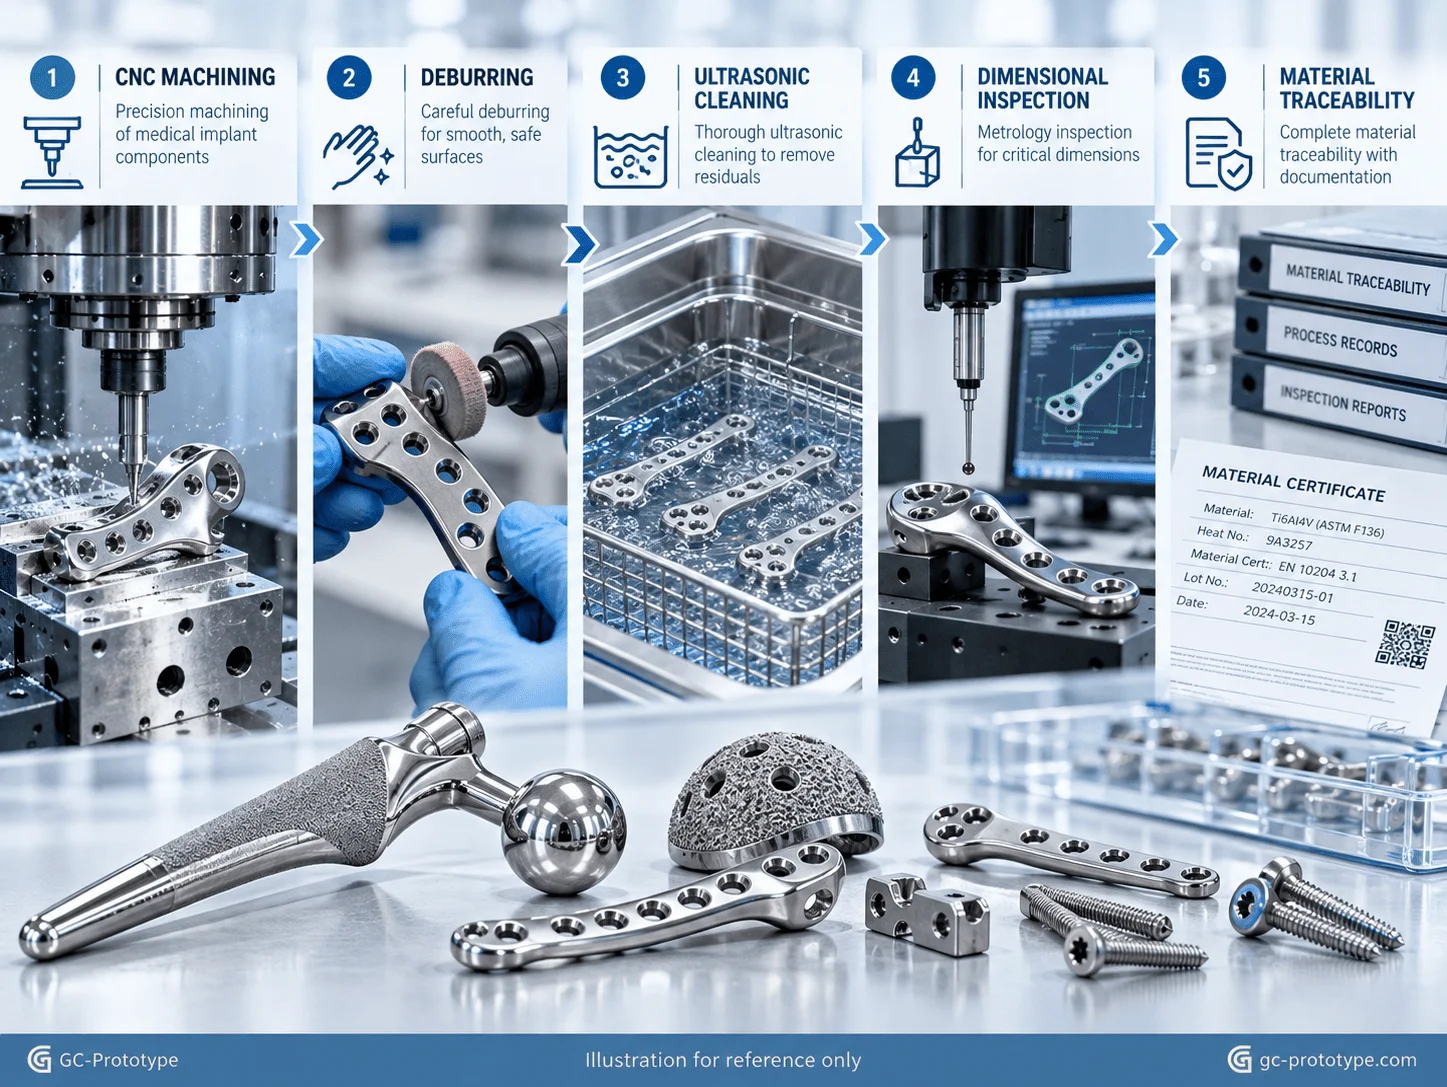
The total cost of a medical implant prototype includes much more than machining time.
Important cost drivers include raw-material certification, setup, programming, cutting time, workholding, inspection, and post-processing.
| Cost Factor | Cost Impact | Optimization Strategy |
| Titanium or implant-grade PEEK | High material cost | Improve stock utilization |
| Complex anatomical surfaces | Longer machining time | Optimize toolpaths |
| Multiple setups | Additional labor | Consolidate operations |
| Extreme tolerances | Higher inspection cost | Prioritize critical features |
| Specialized workholding | Setup investment | Use modular fixtures |
| Surface finishing | Additional processing | Specify functional finishes |
| Quality documentation | Inspection and recordkeeping | Define RFQ requirements early |
For 1–5 prototypes, programming and setup often represent a substantial percentage of the total quotation.
For 10–20 units, those initial costs can be distributed across more components.
However, larger quantities do not automatically justify switching to a different manufacturing process.
Complex implant geometries, regulatory requirements, and product volumes determine whether CNC machining, additive manufacturing, or hybrid manufacturing is more economical.
Procurement teams should request DFM feedback before releasing a prototype order.
Useful questions include:
Can the component fit a smaller stock size?
Can certain features be machined in fewer setups?
Are all specified tolerances necessary?
Can tool access be improved?
Are surface treatments clearly defined?
These decisions can reduce material consumption, unnecessary machining hours, and avoidable rework.
A development team requires a Ti-6Al-4V ELI hip-related component with complex contours and accurately positioned interfaces.
Five-axis machining can support anatomical geometry verification and functional mechanical testing.
A spinal implant designer needs an implant-grade PEEK cage with fixation features and internal openings.
Five-axis CNC machining can support external contouring and accessible internal geometries while maintaining selected critical dimensions.
An orthopedic engineering team requires a curved fixation plate with several angled screw holes.
Five-axis machining may reduce repeated setups and help maintain hole-to-surface positional relationships.
A design based on patient imaging contains irregular external contours and complex geometric interfaces.
Five-axis CNC machining can manufacture accessible surfaces, while additive manufacturing may be more suitable for certain internal structures.
The final method depends on the validated device design.
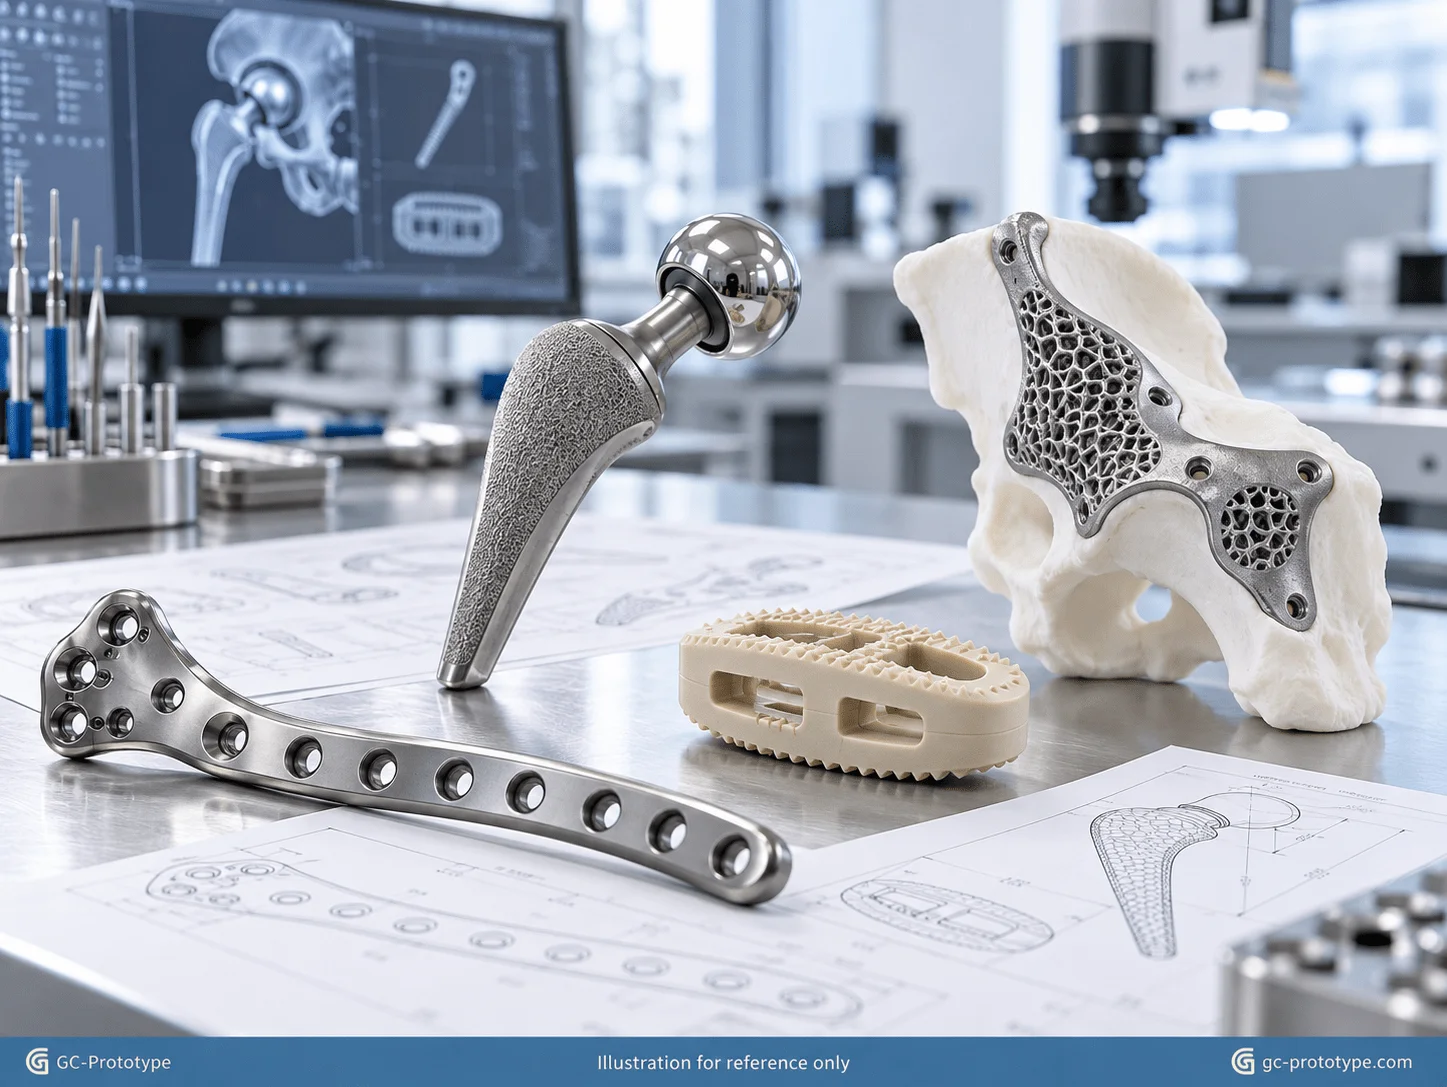
Successful implant development requires coordinated engineering and manufacturing decisions.
The engineering team defines material, geometry, critical tolerances, surface requirements, and inspection expectations.
A DFM review helps identify unnecessary complexity before machining begins.
Initial machined parts allow engineers to evaluate:
Dimensional fit
Anatomical geometry
Assembly interfaces
Functional performance
Representative prototypes may undergo fatigue, mechanical loading, dimensional, or other device-specific validation.
Testing must follow the applicable device-development and regulatory strategy.
Pilot quantities help evaluate manufacturing repeatability, inspection methods, and process documentation.
After design stabilization, manufacturing processes can be optimized for consistency, traceability, cycle time, and production volume.
GC Prototype supports customers across this complete development pathway, helping engineering and procurement teams transition from initial CAD concepts toward production-ready manufacturing.
Five-axis CNC machining improves tool accessibility for complex anatomical surfaces and angled features. It can also reduce repeated setups and help maintain geometric relationships between critical interfaces.
Ti-6Al-4V ELI, commonly called Grade 23, is frequently specified for certain orthopedic implant applications. The exact alloy and material standard must match the intended device requirements.
Selected critical features may achieve this level under appropriate conditions, but capability depends on component geometry, material, tooling, machine stability, and inspection.
Certain appropriately specified implant-grade PEEK materials are used for spinal fusion cages. Suitability depends on material specifications, device design, manufacturing controls, and regulatory evaluation.
Neither process is universally better. CNC machining excels at solid-stock precision components and critical machined interfaces. Metal additive manufacturing is especially useful for complex internal structures and porous designs.
Improve stock utilization, reduce unnecessary setups, optimize tool access, use appropriate internal radii, and apply demanding tolerances only to functional features.
Yes. Precision CNC machining combined with appropriate finishing can produce very smooth surfaces. The required roughness depends on the implant’s intended function and must be verified.
No. ISO 13485 addresses quality-management-system requirements. Device performance and regulatory compliance also depend on the specific design, materials, processes, validation, and applicable regulatory pathway.
An RFQ should include the CAD/STEP model, 2D drawing, exact material specification, prototype quantity, critical GD&T, surface requirements, inspection needs, and documentation expectations.
GC Prototype supports the development pathway from CAD and prototype samples through functional validation, low-volume pilot production, and mass production support.
Five-axis CNC machining provides an important manufacturing solution for orthopedic implants and complex medical hardware requiring anatomical accuracy, demanding tolerances, and reliable material performance.
Through titanium cnc machining for orthopedic implants, development teams can manufacture precise metallic components for engineering validation.
For polymer implant applications, custom peek machining for spinal implants enables the production of complex functional structures using appropriately specified materials.
Understanding 5 axis cnc machining tolerances for medical devices helps engineers establish realistic specifications while avoiding unnecessary machining costs.
Meanwhile, comparing 5 axis cnc prototyping vs 3d printing for implants allows procurement teams to select the most appropriate manufacturing process according to geometry, functionality, cost, and validation requirements.
By combining advanced machining, material traceability, DFM optimization, and controlled quality processes, medical-device teams can reduce manufacturing uncertainty and support more efficient product development.
GC Prototype supports the complete journey from CAD → prototype samples → functional validation → low-volume pilot production → mass production support.
Engineering life-critical medical implants with complex anatomical curves demands exceptional multi-axis accuracy and carefully controlled material integrity. Whether you are a Senior Mechanical Engineer finalizing titanium orthopedic components or a Sourcing Manager evaluating CNC machining versus 3D printing for spinal cages, GC Prototype provides precision machining and manufacturing support.