Address:
Shenzhen Bao'an District Xinqiao Subdistrict Huangpu Community Huangpu East Ring Road No. 504 Shenzhen Yuan Industrial City Building C
Work Hours:
Monday to Friday: 9AM - 21PM
Weekend: 9AM - 21PM
Address:
Shenzhen Bao'an District Xinqiao Subdistrict Huangpu Community Huangpu East Ring Road No. 504 Shenzhen Yuan Industrial City Building C
Work Hours:
Monday to Friday: 9AM - 21PM
Weekend: 9AM - 21PM
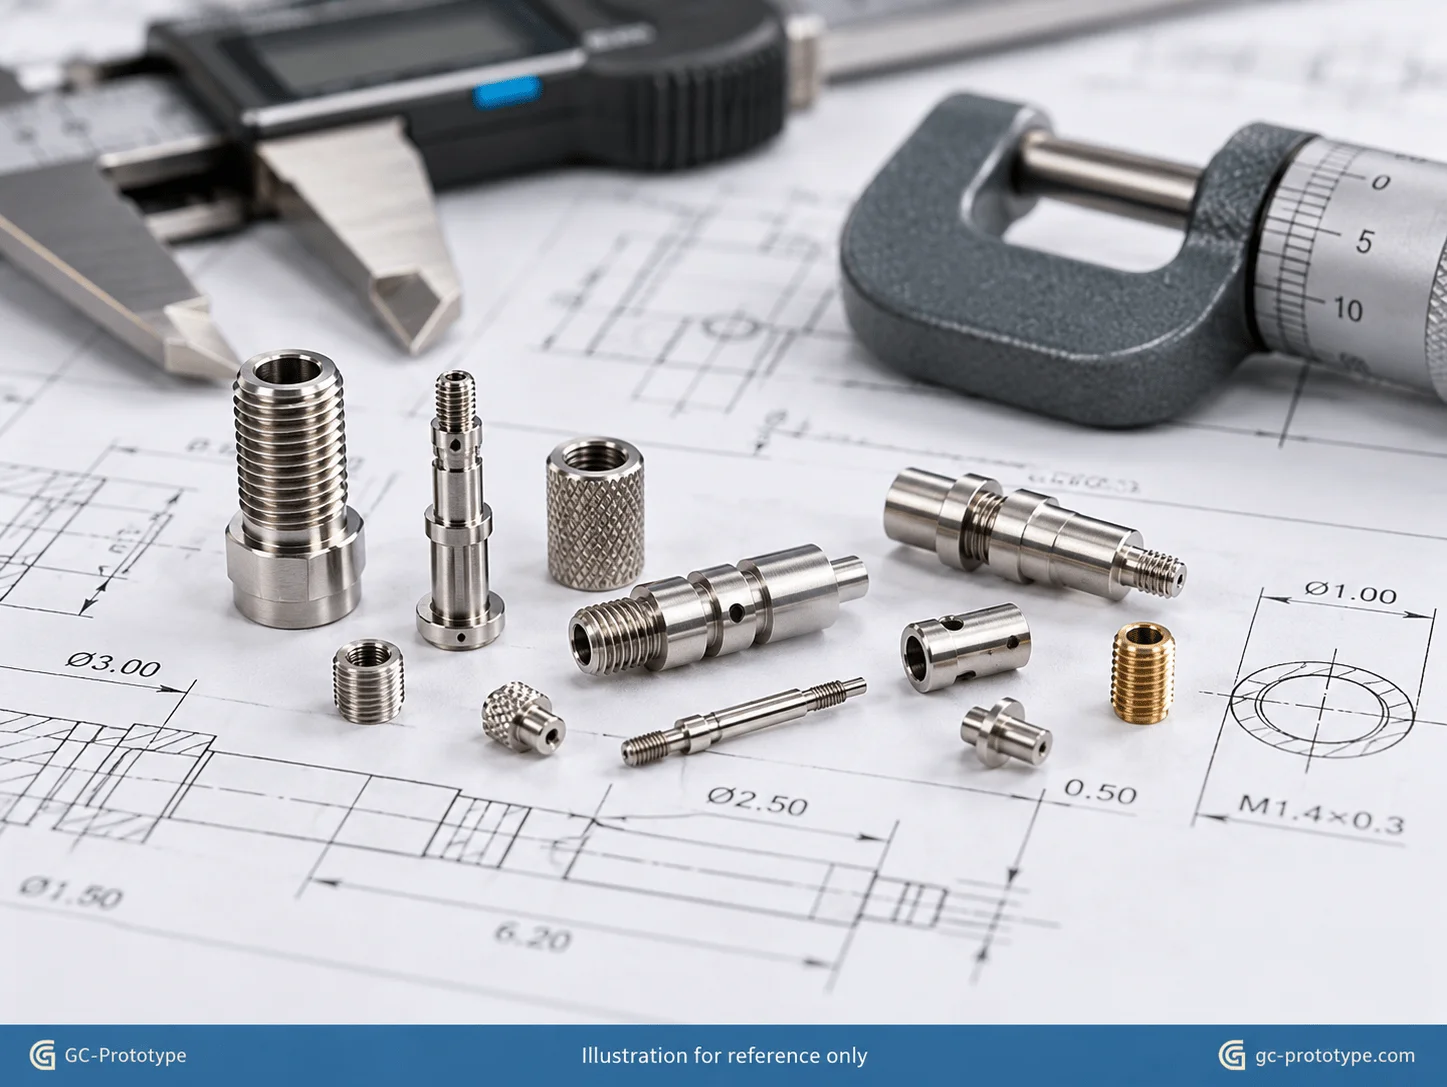
Swiss CNC machining tolerances for medical pins have become increasingly important as medical devices move toward smaller, more complex, and higher-precision mechanical assemblies. For manufacturers developing micro swiss machining for surgical instruments or evaluating swiss machining titanium medical screws, the challenge extends beyond producing miniature parts. Engineers must control concentricity, diameter, surface integrity, burr formation, and material traceability while maintaining reliable performance under demanding medical operating conditions.
During new product introduction (NPI), minimally invasive surgical instruments, orthopedic fixation hardware, endoscopic mechanisms, and fluid-control devices frequently require slender components with extremely tight dimensional relationships. Traditional CNC turning can struggle when long, unsupported workpieces experience bending or vibration under cutting forces.
Swiss-type CNC machining addresses this problem by supporting the workpiece close to the cutting zone. Combined with guide-bushing technology, synchronized machine axes, sub-spindles, and live tooling, it enables complex miniature components to be produced with fewer secondary operations.
For Medical Device Design Engineers, Senior Mechanical Engineers, Manufacturing Engineers, Quality Managers, and Procurement Managers, understanding Swiss machining capabilities is essential to controlling prototype cost and improving manufacturing reliability.
This guide examines surgical applications, titanium material selection, precision tolerances, Swiss versus conventional turning costs, DFM optimization, medical finishing requirements, and the complete manufacturing pathway from CAD → prototype samples → functional validation → low-volume pilot production → mass production support.
Swiss machining, also known as Swiss-type turning or sliding-headstock CNC machining, is a precision manufacturing process designed primarily for small-diameter, elongated components.
Unlike a conventional CNC lathe, where the workpiece is typically held in a fixed headstock chuck or collet, a sliding-headstock Swiss machine advances the bar through a guide bushing while cutting tools operate close to the supported region.
This configuration helps reduce workpiece deflection and improves dimensional consistency, especially for parts with high length-to-diameter ratios.
Consider a miniature surgical pin measuring 2 mm in diameter and 30 mm in length.
Its length-to-diameter ratio is 15:1.
If a conventional lathe supports the workpiece only at one end, cutting forces can cause bending, chatter, and diameter variation.
A Swiss-type machine supports the bar close to the cutting tool, reducing the unsupported length and associated deflection.
Important advantages include:
Improved stability during slender-part turning
Better control of small external diameters
Reduced chatter and taper
Accurate relationships between machined features
Potential for shorter production cycles
Fewer secondary setups on suitably equipped machines
Guide-bushing support does not eliminate cutting forces, and actual accuracy still depends on tooling, machine condition, stock quality, and process control.
Swiss machining is particularly valuable for medical pins, miniature shafts, threaded implants, biopsy-related components, and small surgical instrument mechanisms.
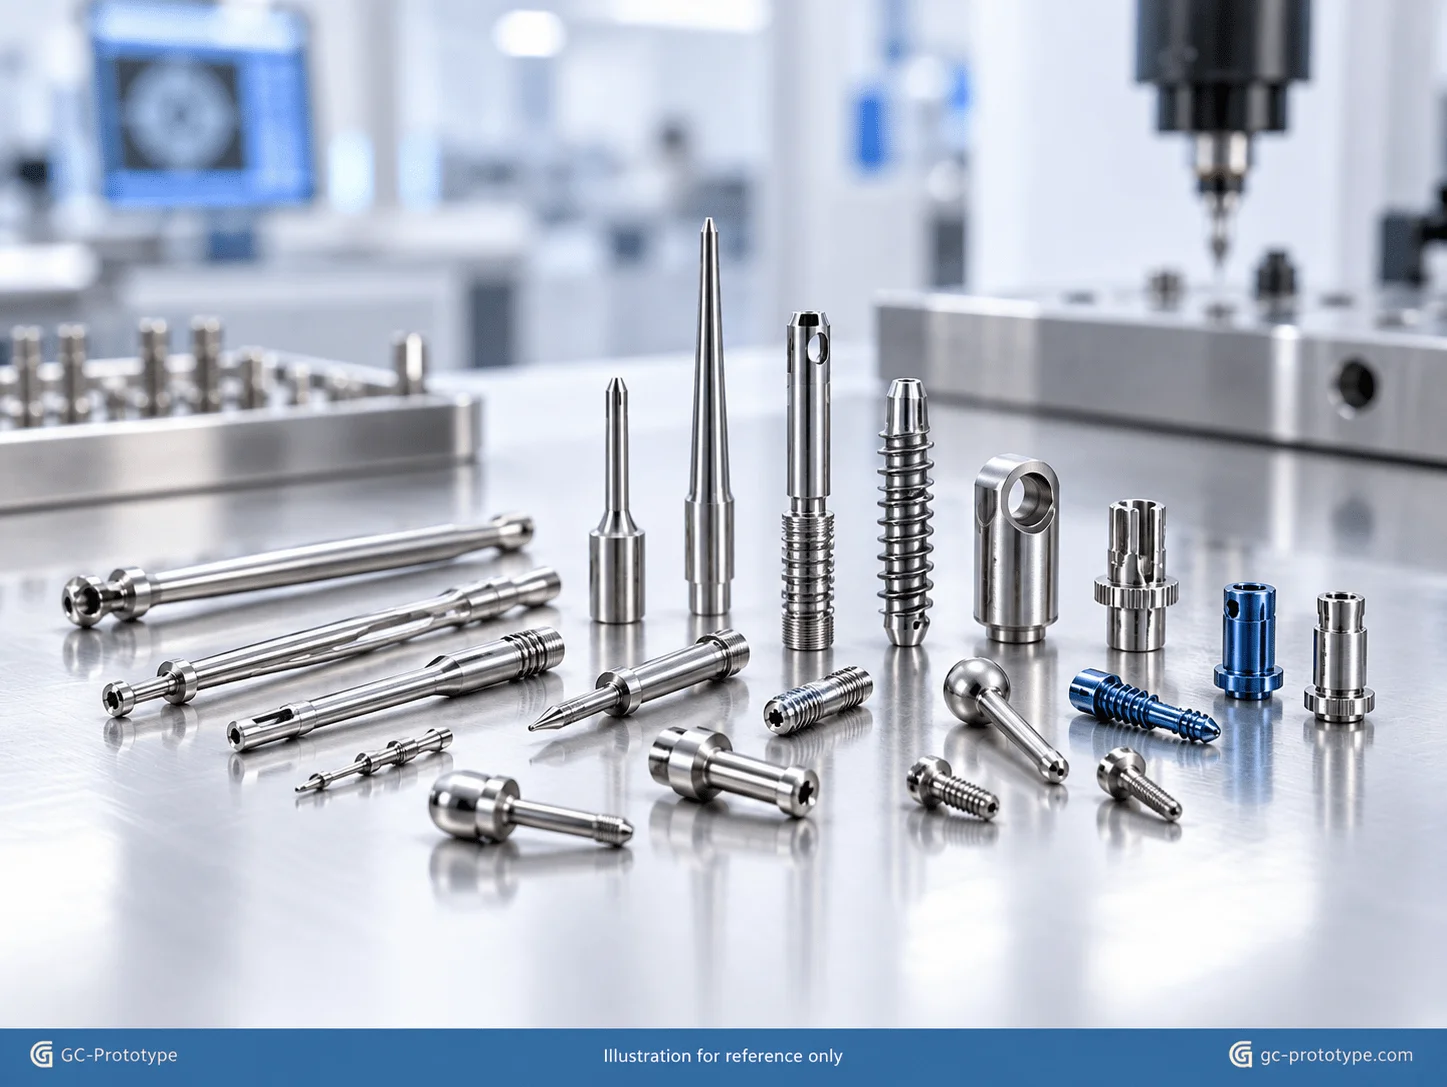
Micro swiss machining for surgical instruments enables manufacturers to produce miniature mechanical features that would otherwise require several machining operations and complex workholding arrangements.
Minimally invasive surgery (MIS) relies on instruments capable of operating through small incisions while maintaining accurate movement and reliable mechanical performance.
Common components include:
Laparoscopic scissor shafts
Endoscopic grasper pivot pins
Biopsy needle components
Miniature drive shafts
Surgical instrument connectors
Precision valve spools
These parts frequently contain complex combinations of cylindrical and noncylindrical features.
A miniature grasper shaft, for example, may require an accurate outer diameter, cross-drilled holes, flats, and precisely positioned slots.
Modern Swiss CNC machines can incorporate high-speed driven tools and synchronized multi-axis motion.
Depending on machine configuration, they can perform:
Cross drilling
Micro milling
Angular flats
Eccentric grooves
Threading
End drilling
without transferring the component to a separate machining center.
This reduces cumulative positioning errors and simplifies manufacturing.
However, features that cannot be accessed from the available tooling positions may still require another setup or process.
Surgical components often contain moving interfaces that repeatedly contact other parts.
Uncontrolled burrs or rough surfaces may contribute to:
Increased friction
Mechanical sticking
Accelerated wear
Inconsistent assembly
For a laparoscopic grasper, even a small burr near a pivot hole can interfere with smooth movement.
Precision machining must therefore consider surface quality and deburring from the beginning.
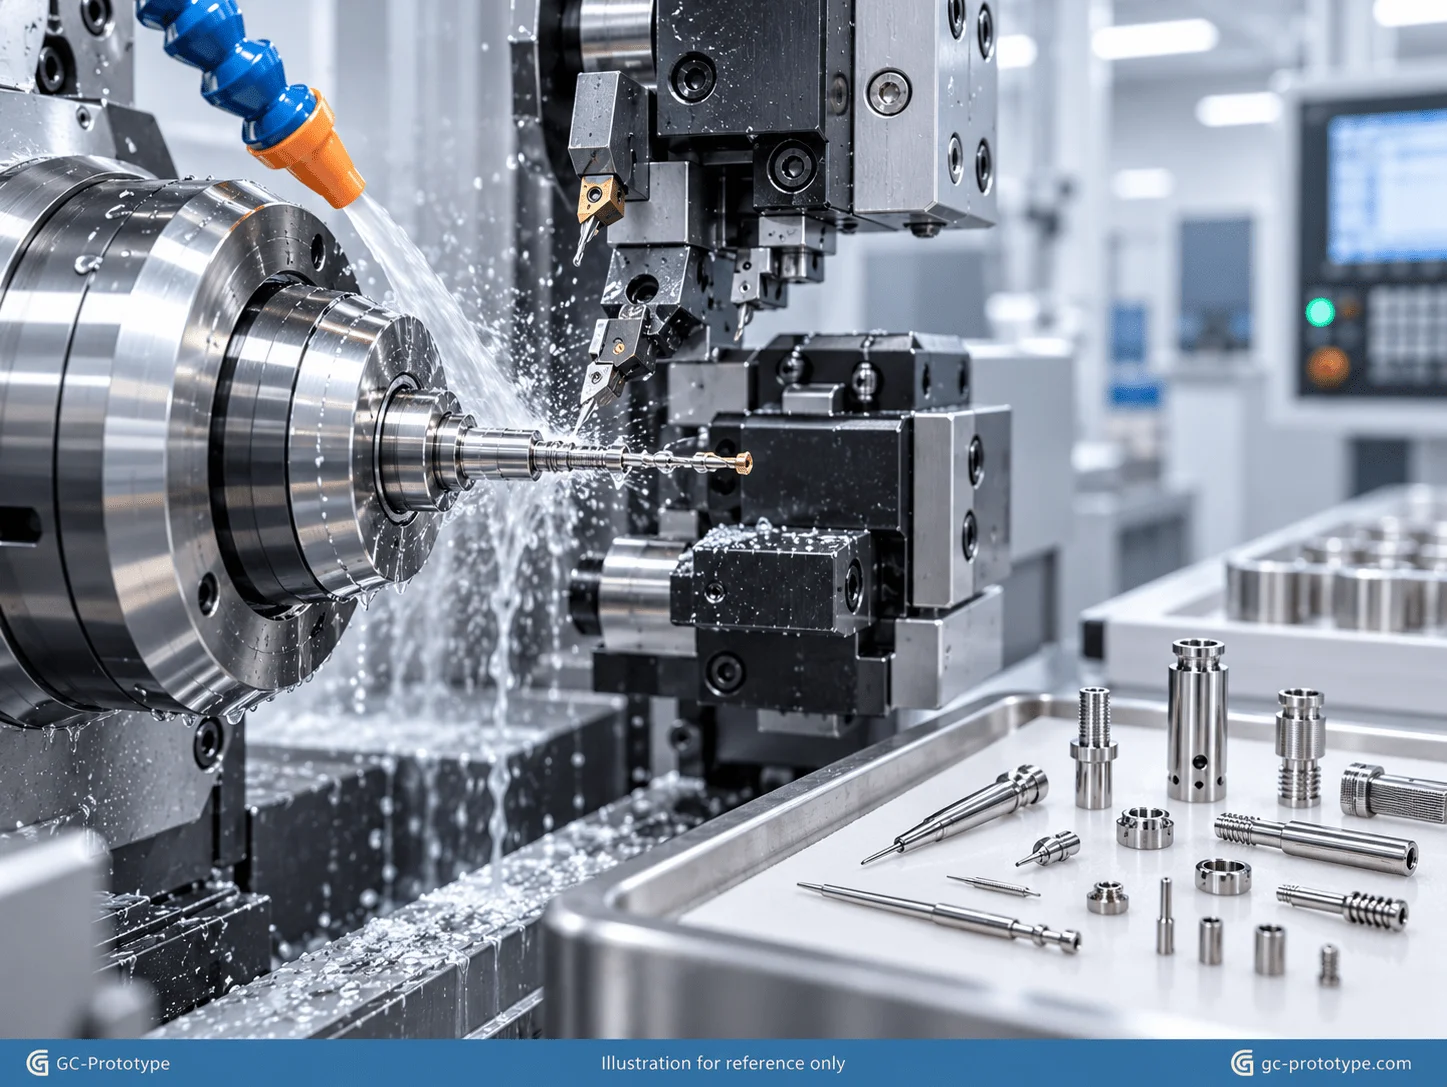
Swiss machining titanium medical screws is especially relevant to orthopedic and dental-device development, where small threaded components must combine accurate geometry with carefully controlled material and surface properties.
Potential applications include:
Cranio-maxillofacial fixation screws
Orthopedic bone screws
Dental abutment components
Miniature fixation pins
Implant-related fastening systems
Ti-6Al-4V ELI, commonly designated Grade 23, is frequently specified for certain implant applications because of its controlled chemistry, mechanical performance, and established use under applicable material standards.
However, selecting Grade 23 does not automatically establish finished-device biocompatibility or regulatory compliance. The exact material specification, manufacturing history, surface processing, cleanliness, and intended clinical use must all be evaluated.
Titanium has relatively low thermal conductivity compared with many conventional machining metals.
Consequently, cutting heat can concentrate near the tool-workpiece interface.
This creates several challenges:
Accelerated tool wear
Adhesion to cutting edges
Burr formation
Surface damage
Dimensional variation
Swiss machining titanium requires carefully selected cutting parameters, stable workholding, suitable cutting-edge geometry, and effective coolant delivery where appropriate.
High-pressure coolant can improve chip evacuation and heat management, but the machining-fluid and cleaning process must be compatible with the medical component’s requirements.
Miniature medical screws may incorporate fine threads, special drive recesses, and small central holes.
The thread design should consider:
Pitch
Root radius
Thread form
Surface finish
Tool clearance
Material removal
Thread quality should be verified using appropriate inspection methods.
The objective is consistent geometry without unacceptable burrs, tears, or surface defects. No machining process can guarantee the absence of microscopic defects without suitable verification.
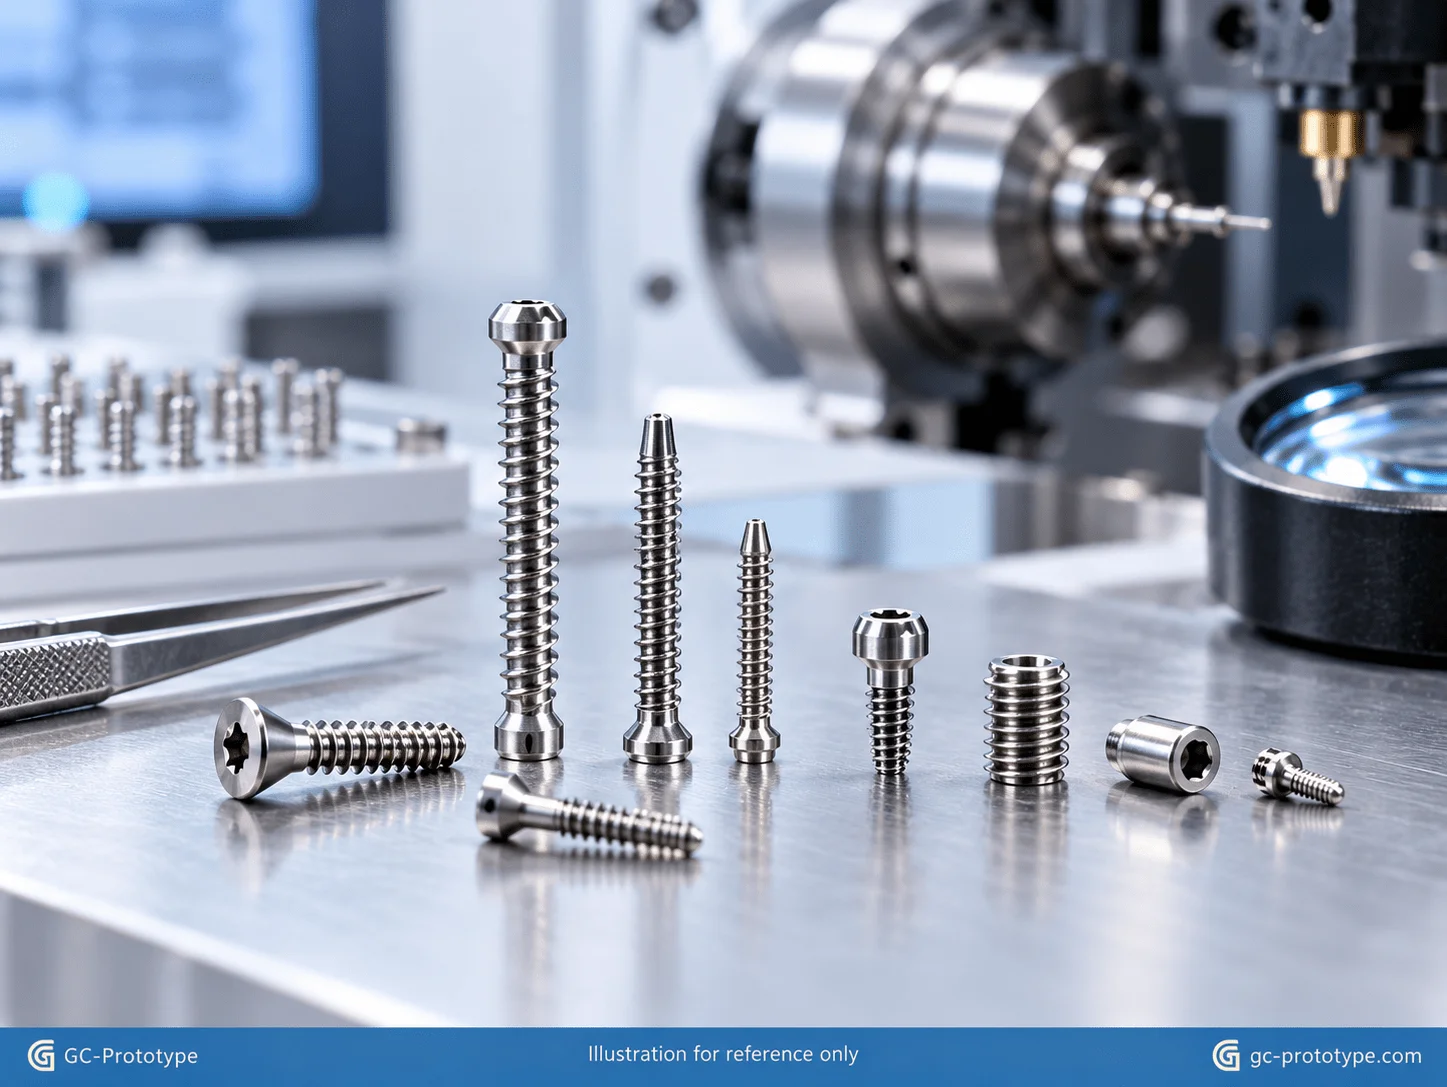
Controlling swiss cnc machining tolerances for medical pins requires an understanding of cutting forces, guide-bushing clearance, machine stability, thermal expansion, and measurement uncertainty.
For slender medical pins, the most important dimensional characteristics may include:
Outer diameter
Roundness
Cylindricity
Straightness
Runout
Surface roughness
The guide bushing supports material close to the cutting edge, reducing the bending associated with longer unsupported workpieces.
This advantage becomes particularly significant when the length-to-diameter ratio exceeds approximately 10:1.
For selected miniature medical features, tolerances of approximately ±0.002–±0.005 mm may be technically achievable under tightly controlled manufacturing conditions.
These values are not standard capabilities guaranteed for every part.
Actual achievable tolerances depend on geometry, material, machine condition, tooling, and measurement capability.
| Feature | Demanding Engineering Target | Important Consideration |
| Outer diameter | ±0.002–±0.005 mm | Feature-specific process capability |
| Roundness | ≤0.003 mm | Workholding and vibration |
| Cylindricity | Drawing dependent | Measurement strategy |
| Straightness | Drawing dependent | Length-to-diameter ratio |
| Surface roughness | Ra 0.2–0.8 µm where specified | Function and tool condition |
Values are illustrative engineering targets, not universal Swiss-machining guarantees.
A critical distinction is that ISO 2768-f general tolerances are not equivalent to ±0.002 mm or ±0.005 mm precision. Such demanding requirements should be specified individually using engineering dimensions and applicable GD&T controls.
Inspection methods may include:
Optical measurement
Laser micrometers
Precision bore gauges
Surface roughness measurement
Optical comparators
Suitable CMM or micro-CMM equipment
The measurement method should be capable of resolving the required tolerance with adequate uncertainty.
For a miniature surgical pin, defining a tight dimension without an appropriate inspection plan creates unnecessary quality risk.
Evaluating swiss machining vs conventional cnc turning cost requires procurement teams to compare total manufacturing cost rather than machine hourly rates alone.
Swiss machines may require more complicated setup and programming, especially when a component uses several driven tools.
However, they can be highly economical for complex miniature components because multiple features may be completed in one coordinated machining cycle.
| Cost Factor | Swiss CNC Machining | Conventional CNC Turning |
| Setup Complexity | Often higher | Often lower |
| Simple Short Parts | Not always economical | Frequently economical |
| Long Slender Parts | Strong advantage | May require additional support |
| Complex Cross Features | Live tooling can combine operations | May require secondary machining |
| Cycle Time | Often competitive for complex parts | Strong for simple geometries |
| Secondary Setup Cost | Potentially lower | Potentially higher |
| Repeat Production | Attractive for suitable components | Attractive for simpler parts |
For 10–100 prototype components, conventional CNC turning may offer a lower initial quotation if the geometry is straightforward.
For 500–10,000 parts, Swiss machining may become more economical when shorter cycle times and fewer secondary operations offset the higher setup investment.
These quantity ranges are useful evaluation scenarios, not fixed economic crossover points.
Consider two hypothetical production plans:
| Cost Element | Swiss Machining | Conventional Turning |
| Initial setup | $600 | $200 |
| Variable cost per part | $7 | $15 |
| 20 parts total | $740 | $500 |
| 100 parts total | $1,300 | $1,700 |
| 1,000 parts total | $7,600 | $15,200 |
These figures illustrate cost structure only; they are not GC Prototype quotations or market price benchmarks.
In this simplified example, the crossover occurs at approximately 50 parts.
Actual results vary significantly according to material, tool life, feature complexity, secondary operations, inspection, and scrap rate.
For sourcing managers, a more useful metric is total landed manufacturing cost, including inspection, finishing, logistics, and quality-related rework.
Medical Swiss-machined parts should be designed with available stock, cutting tools, machine access, and inspection requirements in mind.
Several relatively small design changes can improve manufacturability.
Using commonly available bar diameters can reduce material waste and procurement delays.
A part slightly larger than a standard stock size may require the next larger bar diameter, increasing machining time and cost.
Appropriate thread-relief geometry helps cutting tools exit cleanly.
It can reduce:
Tool-edge damage
Burr formation
Incomplete thread profiles
The relief should be compatible with the intended screw function and applicable design standard.
Critical sliding or rotational interfaces may require micrometer-level dimensional control.
Nonfunctional exterior geometry rarely needs the same tolerance.
Using GD&T to identify essential feature relationships helps focus manufacturing effort where it improves device performance.
Where machine configuration permits, combine turning, drilling, milling, and threading into one setup.
This can reduce:
Secondary handling
Datum transfer
Additional fixtures
Production lead time
Tiny cross holes and intersecting slots can create burrs that are difficult to remove.
Designers should avoid inaccessible sharp intersections when an alternative geometry can provide the same function.
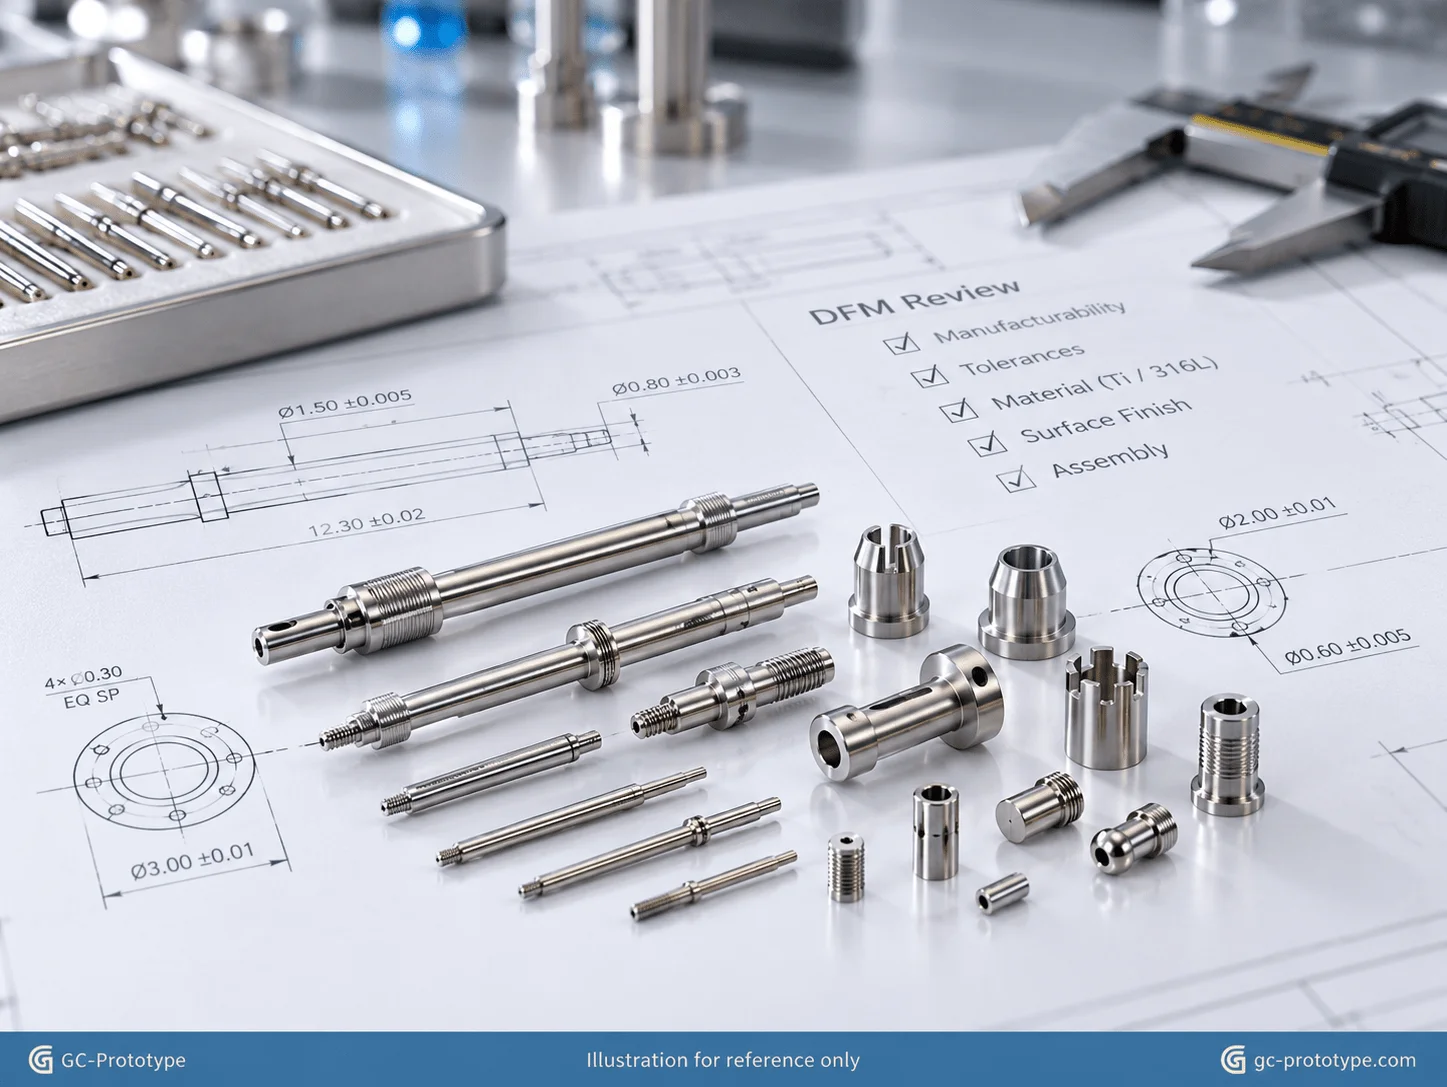
Micro-burrs can compromise the performance of surgical mechanisms, particularly around:
Cross holes
Thread roots
Instrument pivots
Fluid passages
Suitable finishing methods may include controlled mechanical deburring, polishing, or other validated methods.
The process must remove unwanted material without changing critical dimensions.
Citric-acid passivation may be appropriate for specified stainless-steel components under applicable processing standards.
It should not automatically be applied to all titanium or stainless medical parts.
Titanium components may require different cleaning or surface-conditioning processes according to material specification and intended use.
Importantly, passivation alone does not establish biocompatibility or sterility.
Medical-device manufacturers must determine whether additional validation, cleaning, packaging, or sterilization controls are required.
Medical prototype programs may request:
Material certificates
Heat or lot identification
Drawing-revision control
First Article Inspection
Dimensional reports
Surface-finish records
For regulated devices, manufacturers should verify that their suppliers’ quality systems and documented processes satisfy the applicable purchasing requirements.
ISO 13485 certification should only be claimed when independently verified and applicable to the relevant manufacturing organization and scope.
A laparoscopic instrument may contain slender pins that transmit movement to a miniature gripping mechanism.
Swiss machining can produce accurately controlled shaft diameters and integrated features, helping engineers evaluate smooth articulation and repeatable assembly.
Certain biopsy devices use long, narrow metallic components with demanding straightness and surface requirements.
Swiss turning may be appropriate for their precision cylindrical elements, while other processes may be required for final tip geometry or specialized finishing.
Miniature titanium fixation screws need controlled thread geometry and consistent surface quality.
Swiss machines can integrate turning and threading, reducing handling between operations.
A miniature valve spool may require accurately controlled diameters, grooves, and sealing interfaces.
Swiss turning can help maintain dimensional relationships before the component undergoes leak, flow, and functional testing.
GC Prototype supports customers through a complete product-development pathway rather than focusing only on the initial prototype.
Engineering drawings and CAD models are reviewed for material selection, feature accessibility, tolerances, stock dimensions, and machining strategy.
Initial Swiss-machined parts allow teams to verify:
Dimensional fit
Assembly
Mechanical movement
Surface quality
Representative prototypes can then be evaluated through appropriate mechanical, fatigue, fluidic, cleaning, or other product-specific tests.
Pilot quantities help evaluate process repeatability, inspection requirements, and manufacturing costs before larger purchasing commitments.
Once the design is stable, manufacturing planning can focus on tool life, cycle time, quality consistency, documentation, and scalable supply.
This approach helps engineering and procurement teams maintain continuity from the first prototype through production preparation.
Swiss machining is widely suited to small-diameter, slender medical parts such as pins, shafts, screws, instrument mechanisms, and certain valve components.
Selected features may achieve approximately ±0.002–±0.005 mm under controlled conditions. Actual capability depends on geometry, material, machine stability, tooling, and inspection.
The guide bushing supports material close to the cutting tool, reducing unsupported workpiece length and helping control deflection.
Yes. Suitable Swiss machines can produce miniature titanium screws with precision diameters, threads, and additional features, subject to the required material and process controls.
Swiss machining may have higher initial setup costs but lower total cost for certain complex, slender, or repetitive components. The comparison depends on quantity and manufacturing complexity.
Yes. It can be an effective choice for functional prototypes when geometry and precision requirements justify the setup effort.
Manufacturers may use controlled mechanical deburring, polishing, or other validated processes appropriate to the component’s size, material, and dimensional requirements.
No. Passivation may improve corrosion resistance or surface condition for applicable materials, but biocompatibility requires appropriate material and device-specific evaluation.
Examples include stainless steels, titanium alloys, and other materials selected according to the device’s mechanical, environmental, and regulatory requirements.
Include the 3D CAD/STEP file, engineering drawing, material grade, quantity, critical tolerances, surface-finish requirements, inspection expectations, and any traceability or cleaning requirements.
Swiss machining provides an important manufacturing solution for modern medical devices that require small dimensions, complex features, and reliable mechanical performance.
For surgical instrument development, micro swiss machining for surgical instruments can reduce secondary setups and improve the consistency of miniature mechanical features.
For implant-related hardware, swiss machining titanium medical screws enables precision manufacturing of demanding thread and shaft geometries when supported by appropriate material, process, and quality controls.
Engineering teams evaluating swiss cnc machining tolerances for medical pins should focus on real functional requirements rather than applying extremely tight tolerances to every feature.
Procurement managers comparing swiss machining vs conventional cnc turning cost should consider total manufacturing economics, including setup, cycle time, secondary operations, inspection, and production quantity.
GC Prototype supports medical-device development from CAD → prototype samples → functional validation → low-volume pilot production → mass production support, helping teams move from early engineering concepts toward scalable manufacturing.
Engineering miniature medical components with demanding dimensional precision shouldn’t delay your medical-device validation schedule. Whether you are a Senior Mechanical Engineer developing high-aspect-ratio surgical pins or a Sourcing Manager evaluating Swiss machining versus conventional CNC turning, GC Prototype provides precision machining and engineering support for complex miniature components.